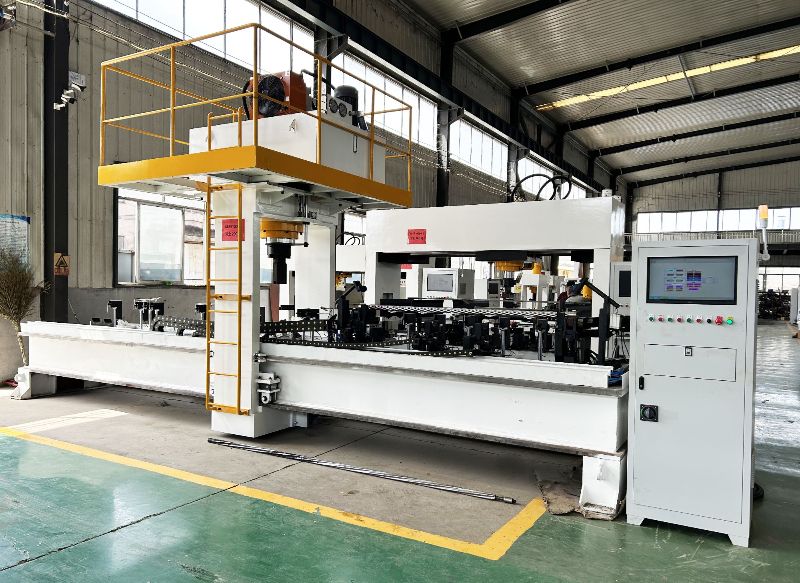
Drill Pipe and Screw Rod Straightening Machine
Shangda configures the machine to your workpiece envelope and throughput target, so pipe length and diameter limits move with your production mix.
View Details →
Explore our complete range of hydraulic straightening machines and accessories.
Shangda configures the machine to your workpiece envelope and throughput target, so pipe length and diameter limits move with your production mix.
View Details →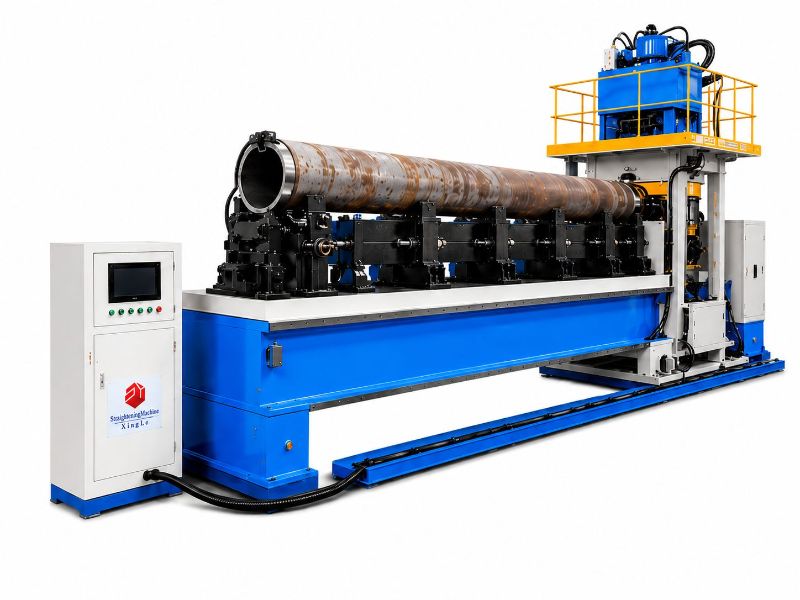
Multi-point laser/vision detection measures deflection at several stations, then a flexible pressure head applies point-pressure straightening.
View Details →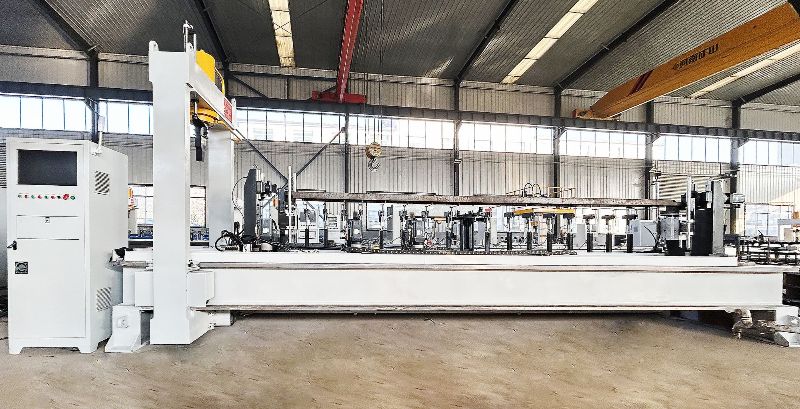
I do not quote a single tolerance for all incoming stock; the machine follows the straightness of the material you feed it.
View Details →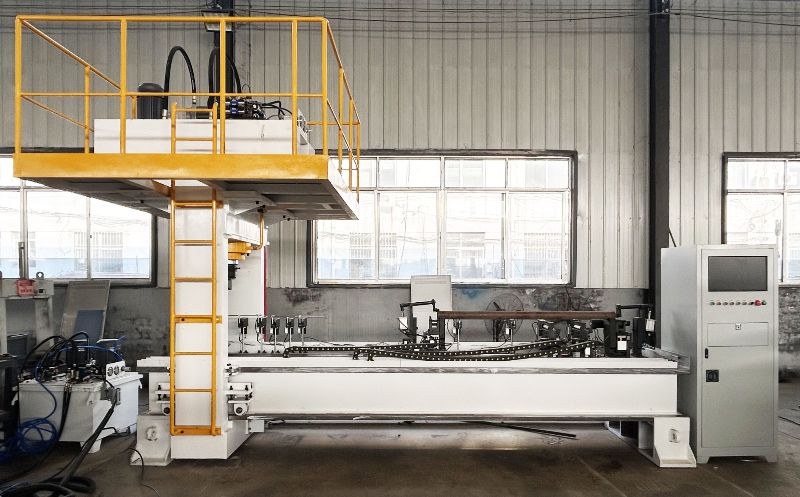
If your incoming rod stock is already straight within 0.3 mm per meter, you can chase tighter output. If it starts with 2 mm of runout, the first pass will correct most of it, not erase it in one shot.
View Details →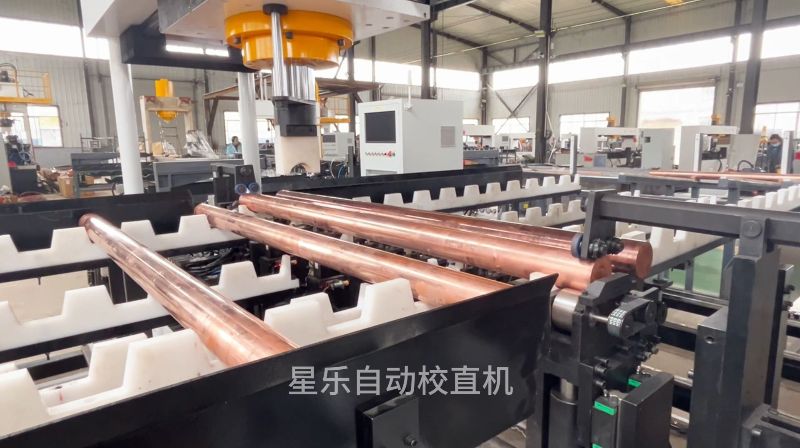
If your copper rod comes in with ovality or residual stress, expect 0.05–0.10 mm after straightening.
View Details →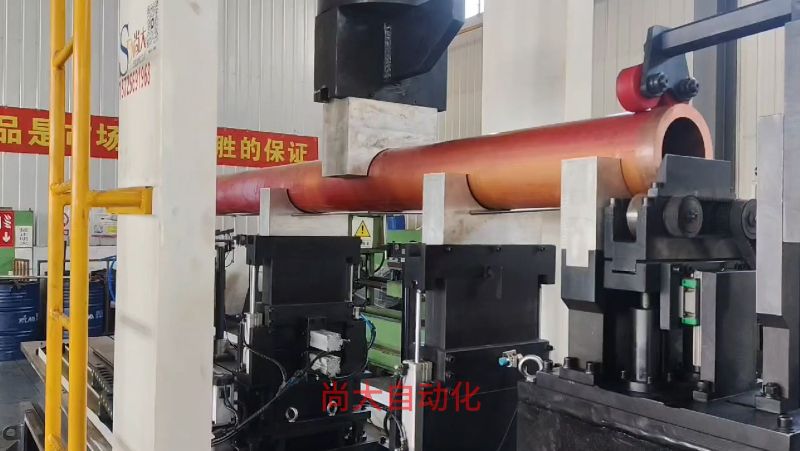
Our copper pipe straightening machine is built for shops that move high volumes of large-diameter tube.
View Details →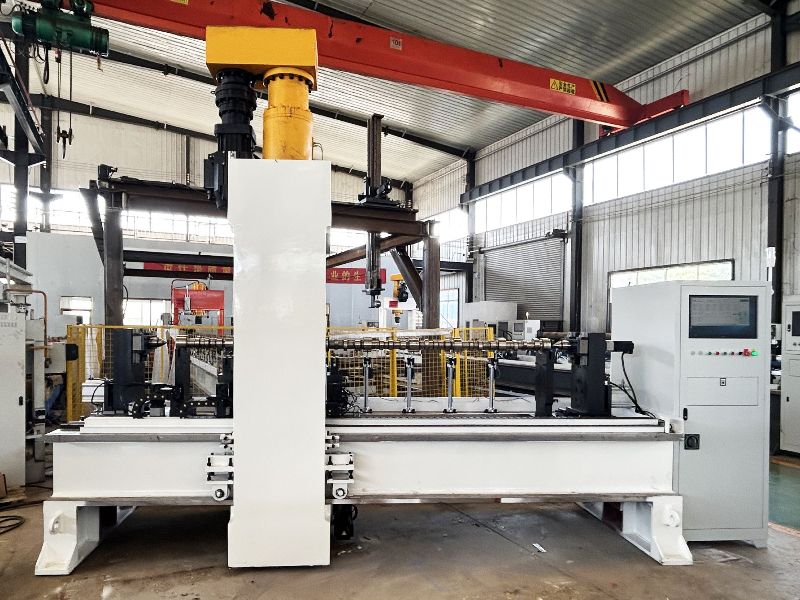
Three to five laser or contact probes scan each shaft before and after every correction.
View Details →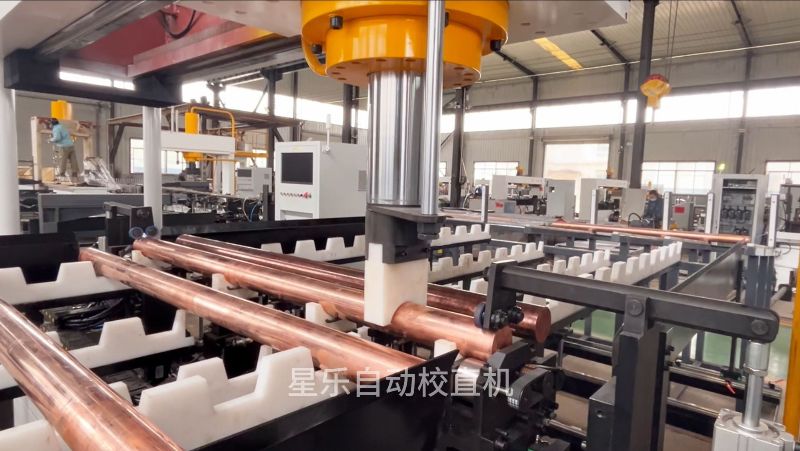
Point-pressure straightening uses flat or contoured anvils so brass rod and tube leave without press marks or scratches.
View Details →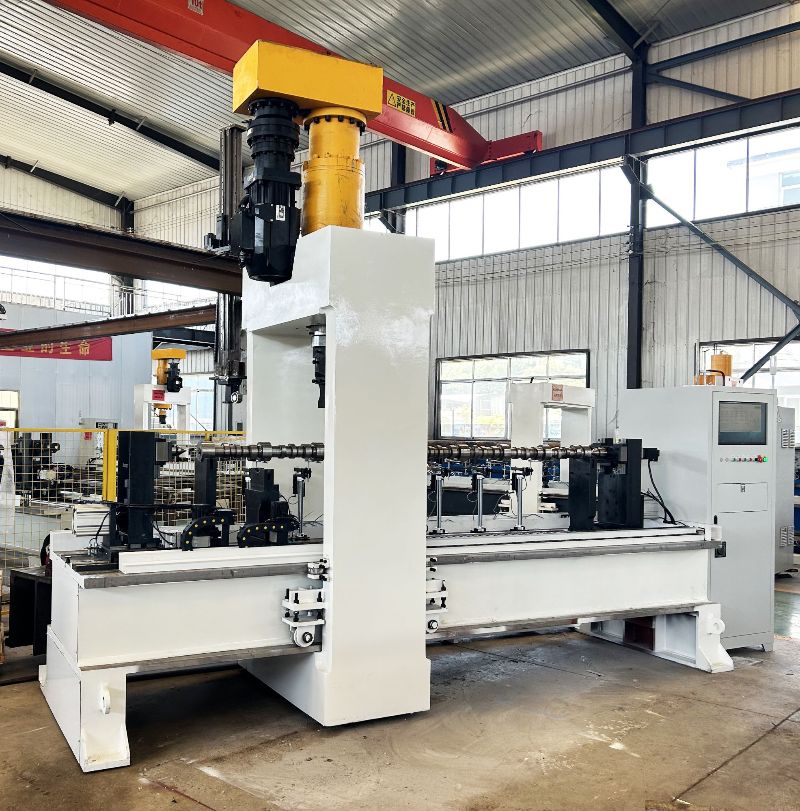
We see this machine used most often on high-volume lines for passenger-vehicle half-shafts and commercial truck axle shafts, where one operator oversees several cells and scrap from a missed spring-back erases a shift's margin.
View Details →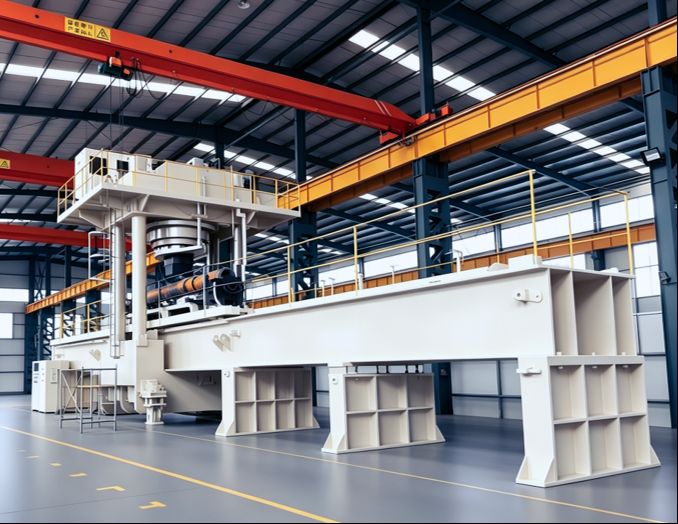
This machine corrects bend without collapsing the cross-section — the problem that separates tube straightening from bar straightening. It handles thin-wall tube that would ovalize in a conventional press and thick-wall tube that needs serious force without cracking the material.
View Details →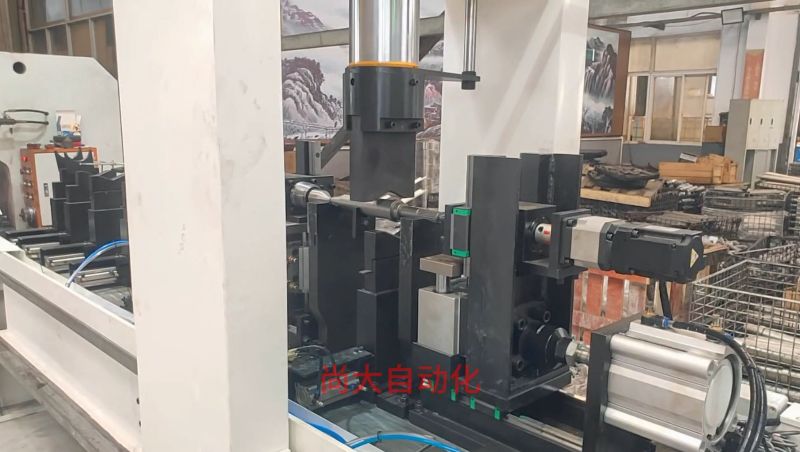
Every shaft brings its own runout signature. A 1,200 mm drive shaft with 0.8 mm initial TIR in the middle needs a different correction strategy than a 200 mm motor shaft with 0.05 mm TIR.
View Details →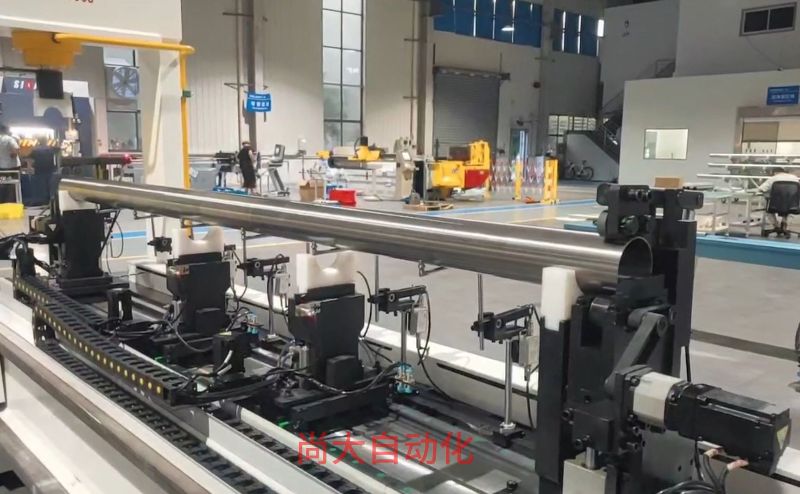
Workpiece material, diameter, wall thickness, cross-section, length, and weight determine the pressure required. Initial deformation and target straightness determine the precision. The machine handles both.
View Details →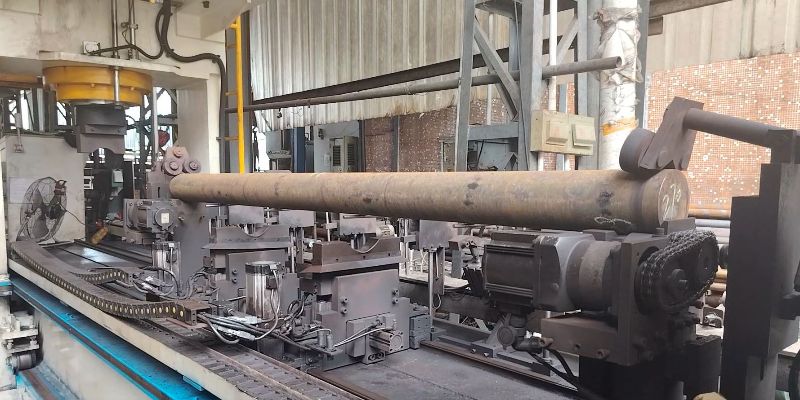
Our straightening line integrates rolling supports, anti-whip guides, and servo-driven measurement to keep the workpiece stable throughout the correction cycle.
View Details →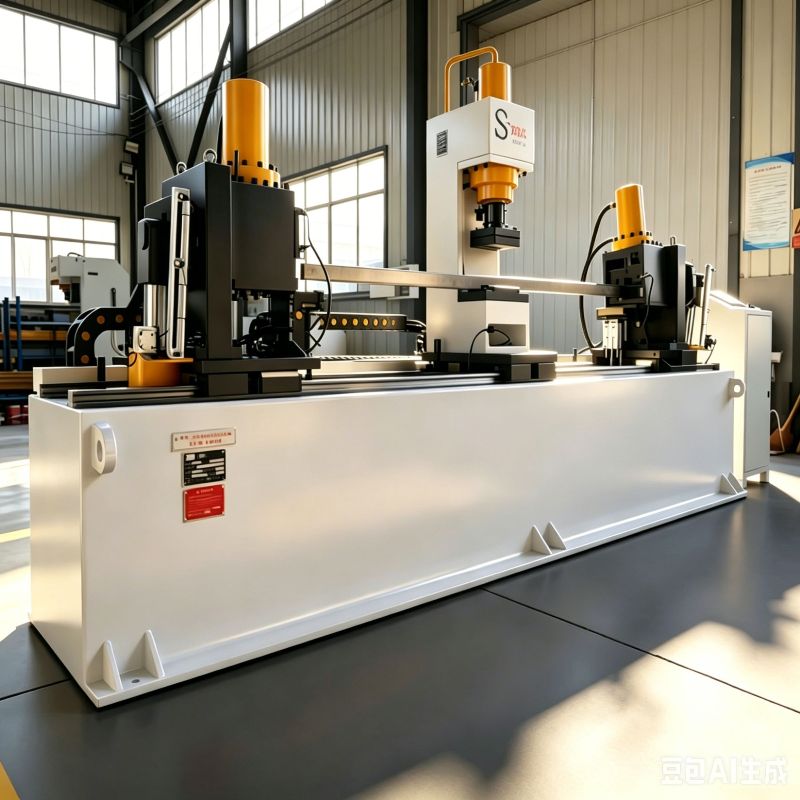
Correct spiral twisting and diagonal bending in square and round tubes — deformation that conventional straightening presses cannot address. 65% of scrapped workpieces recovered to tolerance
View Details →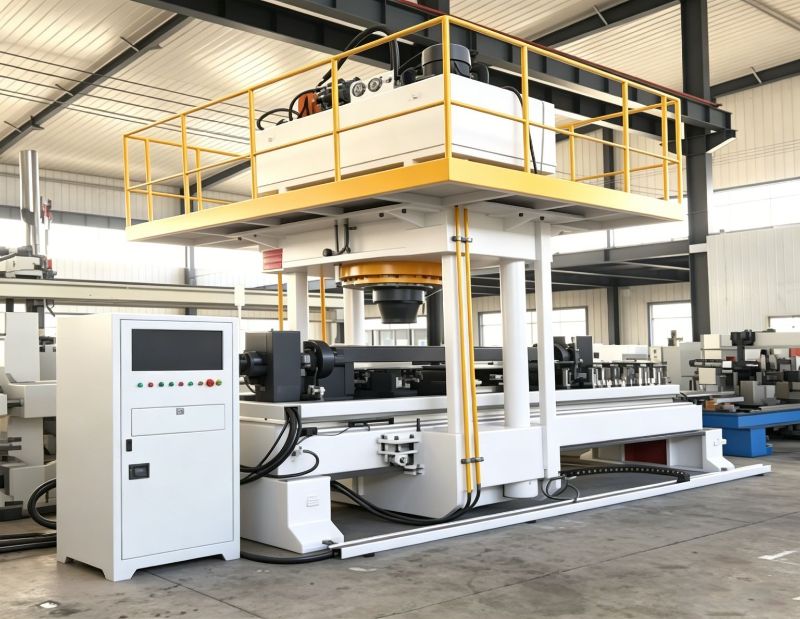
A closed-loop hydraulic straightening system engineered specifically for square and rectangular tube profiles. Multi-point laser measurement, automatic correction cycles completed in 30 seconds to 2 minutes, and straightness control down to ±0.03mm on precision workpieces.
View Details →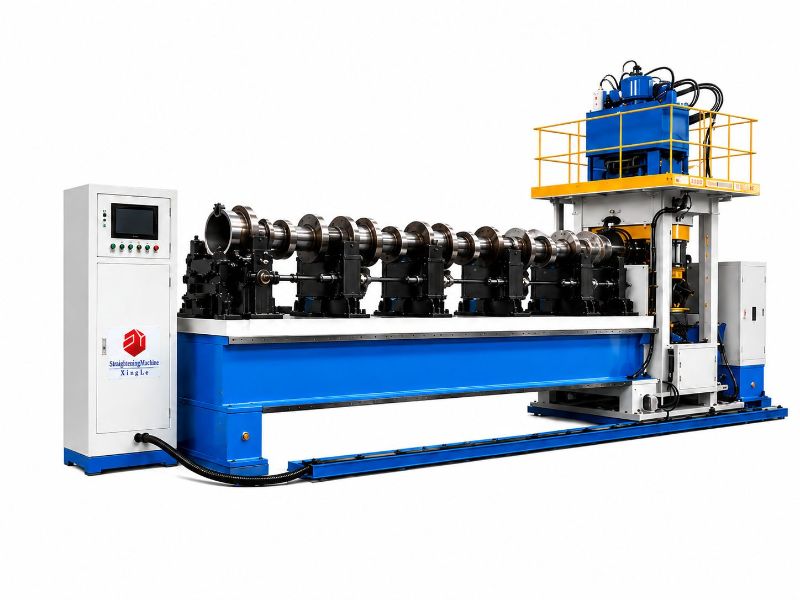
A closed-loop hydraulic straightening press built for high-volume shaft production. Multi-point laser measurement, real-time deflection correction, and automatic loading/unloading combine to deliver ±0.005mm repeatable positioning accuracy with cycle times as fast as 30 seconds per workpiece.
View Details →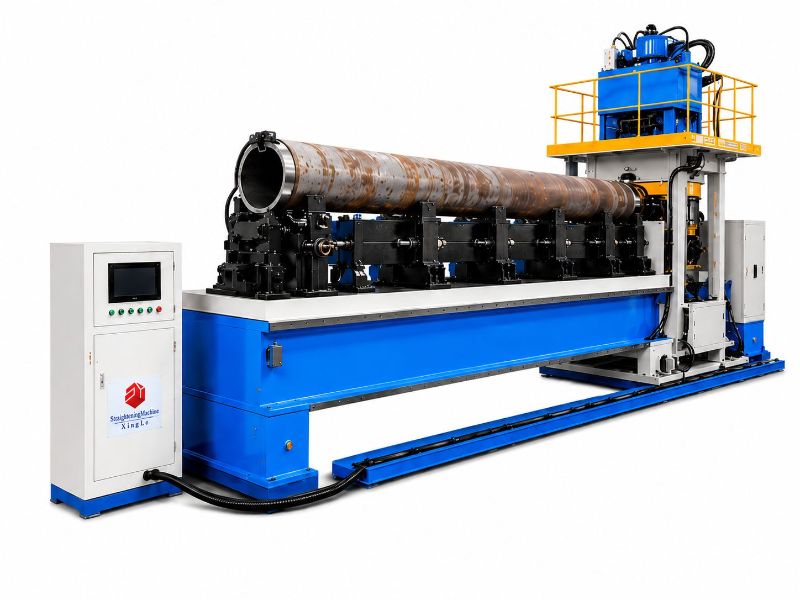
Closed-loop hydraulic straightening for tubes, pipes, and cylindrical workpieces. Multi-point laser measurement with AI-driven force vector correction. Delivers verified straightness down to ±0.01mm across full workpiece length.
View Details →